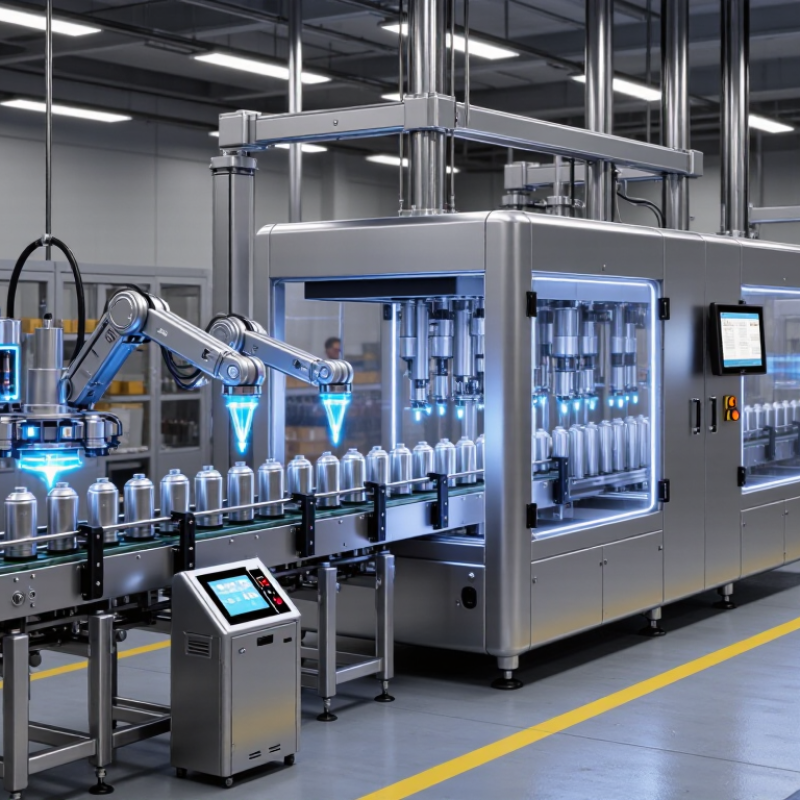
| Sheet Printing Line | Prints decorative graphics and technical information on tinplate sheets before body forming. | Tinplate sheets Aluminum sheets Flat blanks | Commonly configured for several thousand sheets per hour; actual output depends on sheet size, colors, coating, and curing requirements. | Multi-color registration, UV or thermal curing, automatic sheet feeding, coating control, color management, and waste-sheet detection. | Ink and coating systems should comply with the requirements of the intended market and product contact conditions. Electrical guarding and interlocks are essential. | High-volume production of printed aerosol cans with consistent graphics and repeatable color quality. | What sheet sizes and thicknesses are supported? How is color registration maintained? Is operator training included? |
| Can Body-Making Line | Forms flat metal sheets into cylindrical can bodies and joins the side seam. | Three-piece aerosol cans Steel bodies Tinplate bodies | Line speed is selected according to can diameter, height, seam design, and downstream equipment; high-speed systems can operate at several hundred cans per minute. | Automatic blank feeding, body forming, side-seam welding or soldering, seam inspection, body orientation, and automatic rejection. | Pressure-containing containers require controlled seam quality, dimensional inspection, grounding, guarding, and documented process validation. | Manufacturers producing three-piece aerosol cans for household, industrial, personal-care, or automotive products. | What seam technology is used? What are the allowable dimensional tolerances? How are seam defects detected and recorded? |
| Necking and Flanging Machine | Reduces the can diameter at the top and forms the flange required for valve mounting. | Metal aerosol cans Multiple neck profiles Standard valve openings | Usually integrated into automatic lines and rated by cans per minute, with speed determined by the number of necking stages and can dimensions. | Servo-controlled tooling, multi-stage forming, quick die change, dimensional monitoring, automatic lubrication, and jam detection. | Tooling must match the selected valve cup, can diameter, flange geometry, and pressure specification. Guards should prevent access to moving forming parts. | Flexible production of different aerosol can diameters and valve-opening designs. | How many forming stages are required? Are change parts included? What is the changeover time between can formats? |
| Internal Lacquering and Coating System | Applies a protective internal coating to reduce interaction between the formulation and the metal container. | Steel aerosol cans Tinplate cans Specialty coatings | Capacity is normally matched to the can-making line and may range from small batch systems to continuous high-speed production. | Controlled spray or roller application, coating-weight monitoring, drying or curing oven, exhaust ventilation, and coating defect inspection. | Coating selection must be compatible with the formulation, propellant, storage temperature, and regulatory requirements. Solvent handling requires suitable ventilation and fire protection. | Products that may be chemically aggressive or require extended shelf life and corrosion protection. | Can the system handle the required coating chemistry? How is coating weight measured? What curing data will be provided? |
| Pressure Testing Equipment | Checks can integrity, seam performance, and resistance to leakage before filling or shipment. | Empty cans Sealed cans Finished aerosol cans | Available as manual, semi-automatic, or inline systems; test throughput should match the filling and packaging line. | Water-bath testing, air-pressure testing, leak detection, pressure recording, automatic rejection, and traceable test results. | Test pressure, duration, and acceptance criteria must be defined through product specifications and applicable transport or market requirements. | Quality assurance for pressure vessels where leakage or structural failure could create safety risks. | What test method is supplied? Is calibration traceable? Can test results be stored by batch, shift, or serial number? |
| Aerosol Filling Machine | Fills the product concentrate and propellant into the can and crimps the valve assembly. | Liquefied propellant Compressed gas Bag-on-valve products | Common configurations range from low-volume semi-automatic equipment to automatic lines operating at several dozen cans per minute or more. | Accurate concentrate dosing, propellant filling, vacuum or pressure filling, valve insertion, crimp-height control, explosion-protected electrical systems, and automatic shutdown. | Flammable propellants require hazardous-area design, grounding and bonding, gas detection, ventilation, emergency stops, and compliance with applicable local regulations. | Personal-care, household, industrial, medical, and technical aerosol products with controlled filling accuracy. | Which propellants and formulations are supported? What filling accuracy is guaranteed? Does the supplier provide hazardous-area documentation? |
| Valve Crimping Machine | Seats the aerosol valve and forms a secure crimp between the valve cup and can flange. | Standard aerosol valves Bag-on-valve assemblies Metered valves | Often designed for inline operation; practical output depends on valve type, can size, crimp profile, and inspection requirements. | Servo-controlled crimping, adjustable crimp diameter and height, valve presence detection, torque monitoring, and automatic reject handling. | Crimp quality directly affects leak prevention and dispensing performance. Measurement tools should be calibrated and supported by documented setup procedures. | Reliable sealing and consistent aerosol discharge across multiple product formats. | What crimp tolerances are controlled? How is valve misalignment detected? Are sample gauges and setup instructions included? |
| Actuator and Cap Assembly System | Fits the actuator, overcap, protective cap, or spray button after filling and valve crimping. | Plastic actuators Overcaps Protective closures | Typically matched to the filling line and packaging format; modular systems support manual loading or automatic bowl feeding. | Automatic component feeding, orientation control, insertion-force monitoring, presence inspection, cap detection, and quick format changeover. | Components must be compatible with the valve and product design. Guards and interlocks are required around feeding and pressing mechanisms. | High-volume packaging with consistent appearance and secure actuator installation. | Can the system handle different actuator and cap designs? What component tolerances are required? How is missing-part detection performed? |
| Labeling and Coding Equipment | Applies labels or prints batch, date, lot, barcode, and regulatory information on the finished can. | Metal aerosol cans Pressure-sensitive labels Inkjet or laser codes | Available for intermittent or continuous production; rated speed should be confirmed using the actual can diameter, label material, and code content. | Wraparound labeling, vision inspection, barcode verification, tamper-evident application, recipe management, and reject tracking. | Printed information must remain legible throughout storage and distribution. Laser or ink systems must be selected for the substrate and production environment. | Traceable packaging for regulated products and retail or industrial distribution. | Which label materials are supported? Is barcode verification included? Can recipes and production records be exported? |
| End-of-Line Packaging System | Groups, cartons, case-packs, palletizes, and prepares finished aerosol cans for transport. | Retail multipacks Shipping cartons Pallet loads | Configured according to pack pattern, carton size, pallet layout, and required warehouse throughput. | Carton forming, robotic or conventional palletizing, stretch wrapping, case coding, conveyor accumulation, and line-speed synchronization. | Packaging must protect pressure containers from impact, heat, and unauthorized release. Transport packaging should meet the applicable dangerous-goods requirements. | Large-scale distribution where stable packing and automated material handling reduce labor and damage. | What pack patterns and pallet sizes are supported? How are line stoppages managed? Is integration with warehouse systems available? |
| Supplier Engineering Capability | Determines whether the supplier can design and integrate a complete line rather than deliver isolated machines only. | Turnkey lines Modular equipment Retrofit projects | Project duration varies with line complexity, customization, validation, installation, and local approval requirements. | Process layout, utility planning, line balancing, automation integration, factory acceptance testing, site acceptance testing, and documentation. | Supplier should provide risk assessments, electrical drawings, pneumatic diagrams, operating manuals, maintenance schedules, and safety documentation. | Projects requiring coordinated installation, compatibility between machines, and a single technical point of contact. | Who is responsible for line performance? What acceptance criteria are guaranteed? Which utilities, foundations, and site services are required? |
| After-Sales Service and Spare Parts | Supports uptime, maintenance, troubleshooting, upgrades, and replacement of wear components. | Remote support On-site service Preventive maintenance | Service response depends on location, technician availability, remote diagnostics, spare-parts stock, and contractual coverage. | Remote access, spare-parts list, preventive-maintenance plan, operator training, service-level agreement, troubleshooting guides, and software backups. | Critical parts should have defined lead times and approved equivalents. Safety-related repairs must be performed under documented procedures. | Continuous production where unplanned downtime has a significant effect on cost and delivery performance. | What is the guaranteed response time? Which parts are stocked locally? How long will software, controls, and technical documentation be supported? |
| Total Cost of Ownership | Evaluates the full financial impact of purchasing, installing, operating, maintaining, and upgrading the equipment. | Capital cost Energy use Maintenance cost | Should be calculated over the planned equipment life rather than based only on the initial purchase price. | Energy consumption, compressed-air demand, labor requirement, changeover time, scrap rate, spare-parts cost, utilization, and expected service life. | Lower purchase cost should not compromise pressure testing, hazardous-area protection, product quality, or regulatory compliance. | Supplier comparisons where production volume, product variety, and downtime risk materially affect profitability. | What are the guaranteed output, scrap, energy, and maintenance assumptions? Which items are excluded from the quotation? |