Choosing the right Elevator Valve in 2026 requires more than comparing catalog prices. Global buyers must examine pressure ratings, response time, installation conditions, maintenance access, and regional service support. A valve that performs smoothly in a new machine room may struggle in a dusty site, unstable power environment, or high-temperature shaft.
Hydraulic elevator systems commonly use check valves, rupture valves, lowering valves, solenoid valves, and proportional control valves. Each type manages a different risk or movement requirement. Check valves help hold the car securely. Rupture valves limit uncontrolled descent. Proportional valves support gentler starts and stops, especially in premium passenger elevators. Small details matter, such as coil temperature, seal material, manual override design, and emergency lowering behavior.
Michael J. Ryan, a senior hydraulic elevator engineer, puts the purchasing decision simply: “The right valve is not the cheapest part; it is the one that controls motion predictably under pressure.” That principle remains useful for buyers comparing suppliers across Asia, Europe, North America, and emerging markets.
Safety comes first.
Still, no product list can replace site-specific engineering. Flow requirements may be estimated incorrectly. Local technicians may also lack training for advanced electronic valves. This article examines the leading Elevator Valve types for 2026, their practical applications, technical strengths, limitations, and selection criteria. It also considers certification documents, testing records, spare-part availability, and long-term service reliability. Buyers should question attractive specifications. Real performance is often revealed during commissioning, not inside a brochure.
Elevator Valve Basics: Functions, Components, and Operating Principles
Elevator valves regulate hydraulic oil and control the car’s movement. In a hydraulic elevator, the valve block connects the pump, cylinder, tank, and piping. During ascent, oil enters the cylinder through a check valve. The valve closes when the pump stops, preventing unwanted movement. During descent, a lowering valve releases oil at a controlled rate. A pressure relief valve protects the system when resistance becomes excessive. Small parts matter. A blocked filter or damaged seal can create noise, uneven travel, or leakage.
Common elevator valve types include directional valves, flow-control valves, pressure-relief valves, and proportional valves. Directional valves manage oil paths. Flow-control valves adjust descent speed. Proportional valves provide smoother acceleration and leveling by changing flow gradually. Solenoid coils, springs, seals, and adjustment screws support these operations. Buyers should check rated pressure, flow range, coil voltage, oil compatibility, connection size, and local safety requirements. A valve that fits the pipe may still perform poorly with unsuitable oil viscosity.
Tips: Ask for pressure-flow charts, installation drawings, and test records. Inspect the valve block for clean machining and secure fittings. During commissioning, record pressure, travel time, and leveling accuracy. Field experience shows that settings are often copied without checking actual loads. That shortcut deserves reconsideration. A quieter valve is not always a safer valve; stable, repeatable movement matters more.
2026 Top Elevator Valve Types for Global Buyers
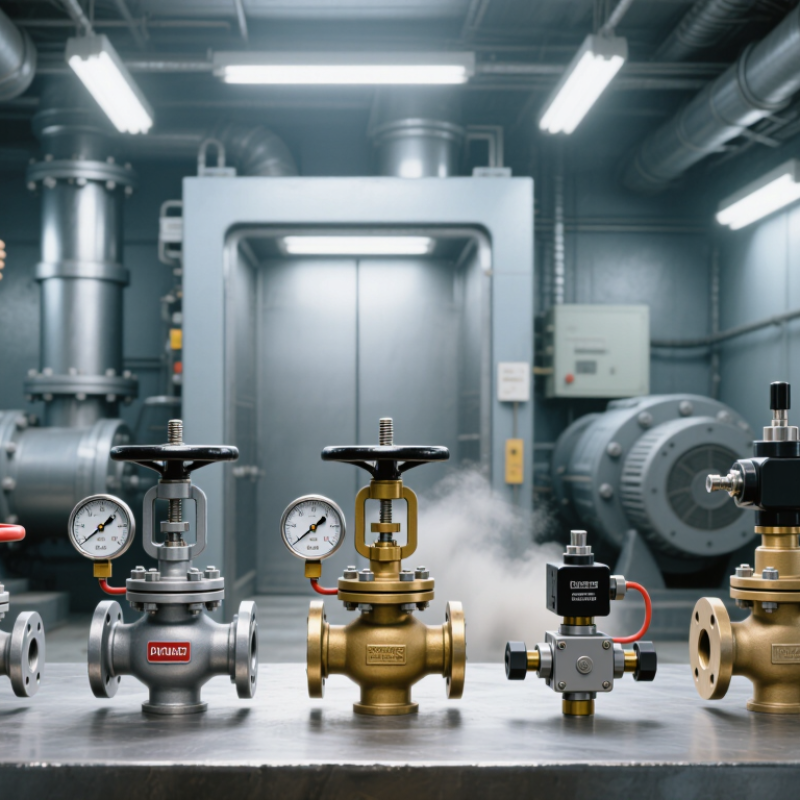
Hydraulic elevator systems use several valve types, each serving a different movement or safety function. The main control valve regulates oil flow between the pump, cylinder, and tank. It supports starting, stopping, acceleration, and leveling. Single-speed valves suit simple, low-rise lifts with limited traffic. Two-speed valves provide separate travel and leveling speeds, improving ride control.
Electronic proportional valves offer finer adjustment for passenger elevators, hospitals, and commercial buildings. Their settings can manage acceleration, deceleration, and floor leveling with greater accuracy.
Check valves prevent reverse oil flow when the pump stops. They are commonly installed near the power unit or cylinder connection.
Rupture valves limit uncontrolled descent if a hydraulic line breaks. They are especially important for lifts with cylinders positioned below or beside the car.
Flow-control valves adjust lowering speed and can help maintain stable movement under changing loads. Emergency lowering valves allow controlled descent during power loss, but their configuration must match the system design. In field inspections, incorrect valve sizing often causes noise, heat, or uneven leveling. Small details matter. Buyers should confirm rated pressure, flow capacity, response time, oil compatibility, and service access. Local elevator codes also matter, including applicable regional standards. A technically suitable valve may still require redesign after site testing. That possibility deserves attention before bulk purchasing.
For 2026 purchasing, global elevator buyers should compare valves beyond catalog flow rates. Hydraulic systems commonly use single-stage, two-stage, and proportional control valves. Each type affects leveling accuracy, ride comfort, response time, and maintenance demands. Small details matter.
A valve performing well at 20°C may react differently in a hot machine room. Check rated pressure, minimum flow, oil viscosity range, and adjustment stability during repeated cycles. Ask for test data, conformity documents, and traceable inspection records. Safety comparison starts with controlled stopping and predictable pressure relief. Verify emergency lowering behavior, fail-safe positions, leakage limits, and protection against unintended movement.
Compatibility is equally practical. Confirm port size, mounting orientation, coil voltage, controller signals, seal materials, and hydraulic fluid. Even a technically strong valve can create delays when replacement parts are unavailable locally. Local elevator codes and qualified installation practices must guide the final selection. Do not rank valve types by price alone. Compare service cost, adjustment time, noise, energy use, and spare-part access. During commissioning, record stopping distance, floor leveling, temperature, and pressure readings. Repeat measurements with loaded and empty cars. That evidence exposes weak assumptions. I would not treat one successful test as proof of universal compatibility. Real shafts vary, and field conditions are often less tidy than specifications.
For global buyers, elevator valve selection starts with compliance, not catalog variety. Hydraulic systems commonly use lowering valves, check valves, shutoff valves, flow-control valves, and rupture-valve protection. Each type affects descent speed, pressure stability, and emergency stopping. During inspections, technicians often check valve markings, pressure ratings, connection sizes, and access for manual testing. Small details matter.
A 2024 Fortune Business Insights report estimated the global elevator and escalator market at about USD 88.6 billion in 2023. This expanding market increases demand for documented, interchangeable hydraulic components. Buyers should request test reports, material certificates, calibration records, and installation instructions. EN 81-20 and EN 81-50 are important references for many European projects. ASME A17.1/CSA B44 applies in North American jurisdictions. ISO 4413 also provides useful hydraulic safety principles.
Certificates alone are not enough. They may not cover the exact valve configuration, pressure range, or installation environment. Check whether the product supports the required safety function under abnormal pressure or power loss. For European supply chains, pressure equipment requirements may also apply. Local authorities can impose additional rules.
Field experience shows that mismatched seals often create leakage after temperature changes. That risk is easy to underestimate. A buyer should compare fluid compatibility, response time, noise, and maintenance access. The process is not perfect, especially when regional standards overlap. A careful technical review remains necessary before approval.
2026 Top Elevator Valve Types for Global Buyers
2026 Purchasing Criteria: Suppliers, Costs, and Long-Term Maintenance
Global buyers commonly compare hydraulic control valves, rupture valves, check valves, and lowering valves. Each type serves a different safety or motion-control function. Hydraulic systems need valves that manage oil flow smoothly during starting, stopping, and emergency lowering. Traction elevators use fewer hydraulic components, but brake and pressure-control assemblies still require precise inspection.
Supplier quality affects the real purchase cost. Request material certificates, pressure-test records, dimensional drawings, and replacement-part lists before ordering. A reliable supplier should explain seal materials, operating temperature, delivery limits, and technical support. The lowest quotation can hide poor documentation or expensive downtime. Compare the full lifecycle cost, not only the invoice. Include freight, installation labor, oil contamination checks, spare seals, and technician training. Regional service availability matters.
Maintenance planning should begin before installation. Record the valve model, pressure settings, installation date, and inspection results. Check for oil leakage, slow platform leveling, unusual noise, and unstable pressure. Small leaks become costly problems. No checklist is perfect. Buyers may also misjudge long-term availability when selecting a rare valve configuration.
Tips: Choose standardized connections when possible. Keep two seal kits in stock. Confirm compatibility with local voltage, oil type, and safety requirements. Ask for a written maintenance interval, but adjust it after reviewing actual site conditions. A dusty machine room or frequent cycling may require earlier inspections.
Practical comparison of commonly specified hydraulic elevator valve configurations. Cost figures are indicative 2026 international purchasing ranges for the valve assembly only and vary by capacity, certification, control options, order quantity, and shipping terms.
| Valve Type | Typical Application | Typical System Capacity | Control Method | Indicative Purchase Cost (USD per valve assembly) |
Energy and Ride Characteristics | Maintenance Profile | Key 2026 Buying Criteria |
|---|---|---|---|---|---|---|---|
| Single-Stage Hydraulic Valve | Low-rise residential buildings, small commercial lifts, and basic goods or accessibility elevators. | Commonly up to approximately 1,000 kg and 0.15–0.30 m/s, depending on the complete hydraulic system. | Mechanical or solenoid-operated on/off control with basic acceleration and deceleration adjustment. | $350–$1,000 | Lowest initial cost. Ride comfort is acceptable when correctly adjusted but is generally less precise than multi-stage or electronic control. | Simple to diagnose and repair. Periodic inspection of seals, solenoids, filters, pressure settings, and oil cleanliness is required. | Confirm pressure range, port size, oil compatibility, manual emergency lowering, replacement seal availability, and local service capability. |
| Two-Stage Hydraulic Control Valve | Passenger elevators in low- and mid-rise buildings where smoother starting and stopping are required. | Commonly 450–2,000 kg and approximately 0.15–0.60 m/s. | Separate high-speed and leveling-stage flow control, normally using hydraulic adjustment and solenoid functions. | $700–$1,800 | Better leveling and stopping performance than a basic single-stage valve; moderate energy efficiency when properly tuned. | Requires periodic adjustment of acceleration, deceleration, leveling speed, and pressure. Contaminated oil can cause unstable performance. | Evaluate repeatable leveling accuracy, adjustment range, valve response time, coil voltage, spare-part lead time, and commissioning support. |
| Multi-Stage Soft-Stop Valve | Passenger elevators serving apartments, hotels, hospitals, and offices where ride comfort is a priority. | Commonly 630–2,500 kg and approximately 0.30–0.80 m/s. | Multiple hydraulic stages regulate start, acceleration, high-speed travel, deceleration, leveling, and stop. | $1,000–$2,500 | Smooth acceleration and stopping with reduced pressure shock, lower vibration, and improved passenger comfort. | More adjustment points than basic valves. Preventive maintenance should include filter replacement, pressure verification, and calibration records. | Request ride-quality test data, allowable temperature range, pressure-loss data, tuning instructions, and technician training materials. |
| Electronic Proportional Valve | Premium passenger elevators, modernization projects, and installations requiring precise speed and leveling control. | Commonly 630–3,000 kg and approximately 0.30–1.00 m/s, subject to the complete hydraulic power unit. | Electronic controller and proportional solenoid regulate oil flow continuously or in fine increments. | $1,800–$4,500 | Excellent ride quality and leveling accuracy. Efficient control is possible, but electrical and hydraulic system matching is essential. | Requires qualified technicians, electrical diagnostics, sensor checks, software or parameter backup, and clean hydraulic oil. | Check voltage stability, electromagnetic compatibility, controller interoperability, parameter access, cybersecurity of connected controls, and long-term electronics support. |
| Emergency Lowering and Manual Rescue Valve | Passenger and goods hydraulic elevators requiring controlled descent during power failure or emergency evacuation. | Selected according to cylinder pressure, rated load, flow rate, and emergency-lowering requirements. | Manual hand pump, mechanical release, electrically actuated emergency lowering, or a combined arrangement. | $250–$1,200 | Does not improve normal travel performance; provides controlled movement to a safe landing point during specified emergency conditions. | Functional testing is essential. Inspect manual controls, batteries where fitted, release mechanisms, hoses, seals, and tamper protection. | Verify fail-safe operation, emergency flow limitation, compatibility with the lift controller, accessibility of controls, and applicable local safety rules. |
| Rupture or Hose-Burst Safety Valve | Hydraulic elevators requiring protection against uncontrolled descent caused by a damaged hose or sudden excessive oil flow. | Selected by cylinder connection, rated load, design pressure, and required trip flow. | Hydraulic flow-activated shutoff or restriction; normally passive during normal operation. | $150–$650 | No direct effect on normal energy use when correctly sized; provides a protective shutdown or flow restriction during abnormal conditions. | Inspect for leakage, contamination, incorrect installation direction, damaged threads, and evidence of unintended activation. | Confirm certified flow setting, pressure rating, connection dimensions, reset procedure, inspection access, and compatibility with the cylinder and hose. |
| Pressure Relief and Anti-Creep Valve Assembly | Systems needing protection from excessive pressure and reduced unintended car movement while parked. | Selected according to pump flow, working pressure, cylinder size, and required holding performance. | Pressure relief, check, pilot-operated, or combined hydraulic functions. | $300–$1,200 | Supports system protection and stable holding. Poor adjustment can cause heat generation, noise, leakage, or leveling drift. | Test pressure settings and check for internal leakage. Oil cleanliness and correct relief adjustment are critical. | Compare pressure stability, relief repeatability, leakage limits, test-port accessibility, seal materials, and adjustment protection. |
| Integrated Hydraulic Elevator Valve Block | New installations and modernization projects seeking a compact assembly combining several control and safety functions. | Commonly 450–3,000 kg; final suitability depends on flow, pressure, speed, and cylinder arrangement. | Integrated mechanical, solenoid, proportional, check, relief, and emergency functions in one engineered block. | $1,200–$5,000 | Compact layout can reduce pressure losses, tubing, installation time, and leakage points when correctly engineered. | Fewer external connections but more specialized parts. Repairs may require a complete cartridge, coil, or valve-block service kit. | Review hydraulic schematic, replaceable cartridge design, service clearances, spare-module cost, commissioning procedure, and documentation quality. |